How procurement planning reduces supply risk in Latin America
A production schedule can look secure until one imported component stops at a port, a gas shipment requires a document that was not requested early enough, or a qualified supplier cannot confirm the exact lot available for release. In Latin America, these disruptions are especially costly when the purchase supports semiconductor work, aerospace machining, medical-device production, advanced coatings, or precision metrology. The immediate issue may appear to be a late delivery, but the underlying failure often began much earlier: procurement was treated as an order-placement task rather than a risk-planning process.
Procurement planning reduces supply risk in Latin America by turning uncertain supply conditions into visible decisions before production depends on them. It connects demand forecasts, technical specifications, supplier qualification, trade documentation, transport routes, inventory policy, and contingency sourcing. Instead of asking only whether a supplier can quote a part, buyers evaluate whether the complete supply path can reliably deliver the approved item, in the required condition, with the documentation needed for acceptance and use.
Why reactive purchasing creates larger problems in the region
Urgent buying can work for standard consumables with multiple local distributors. It becomes far less reliable when the requirement involves ultra-high-purity chemicals, electronic gases, thin-film deposition inputs, precision pneumatic components, coordinate measuring equipment, sensors, motion stages, or custom-machined assemblies. These items may have limited production slots, controlled shipping conditions, lengthy calibration requirements, or export-review considerations.
A procurement team may receive an acceptable unit price and still inherit a serious supply exposure. The quoted lead time might start only after technical approval. The equipment could require packing suitable for vibration-sensitive optics. A chemical shipment may need packaging, labeling, safety documentation, or local import handling that the buyer has not accounted for. Spare parts may be supplied from a different country than the main system, creating a separate customs and transit risk.
Latin America is not a single procurement environment. Port capacity, inland transportation, customs procedures, local representation, foreign-exchange controls, tax treatment, and documentation expectations can differ substantially by country and even by shipment type. Planning does not eliminate those differences. It prevents them from being discovered after a production commitment has already been made.
Start with the requirement that actually drives risk
The first planning task is to separate the commercial request from the operational requirement. A purchase requisition that says “source equivalent valve” or “buy high-purity process gas” is not sufficient for critical procurement. The team needs to establish which characteristics are fixed, which can be substituted, and which must be approved by engineering, quality, environmental health and safety, or regulatory personnel.
For high-precision supply chains, the most important requirement fields often include:
- Part number, revision level, drawing status, and approved material or coating specification.
- Purity grade, contamination limits, cylinder or container configuration, and shelf-life limits for chemicals and gases.
- Measurement uncertainty, calibration traceability, software compatibility, and environmental limits for metrology equipment.
- Pressure range, response behavior, seal material, media compatibility, and cleanliness class for pneumatic or fluid-control components.
- Packaging, shock protection, temperature limits, moisture protection, and handling restrictions during transport.
- Required certificates, safety documents, inspection records, origin information, and any end-use documentation needed before shipment.
This definition work may seem slow at the beginning, but it avoids a common failure mode: a supplier ships a commercially similar item that cannot be installed, validated, cleared, stored, or released to production. The most expensive shortage is not always a missing part. It can be an item physically present at the site but unusable because its identity, condition, or documentation cannot be verified.
Build a supply map, not just a supplier list
A supplier list tells buyers who can sell an item. A supply map shows where risk can interrupt delivery. For each critical category, map the manufacturing location, final testing location, export point, freight route, customs entry point, domestic delivery route, local service capability, and any distributor that takes legal or physical possession of the goods.
This exercise is particularly useful for imported technical products. A metrology system may be built in one facility, calibrated elsewhere, exported through a third country, and supported locally by a representative that does not stock critical replacement modules. Without a supply map, the buyer may assume local representation equals local availability.
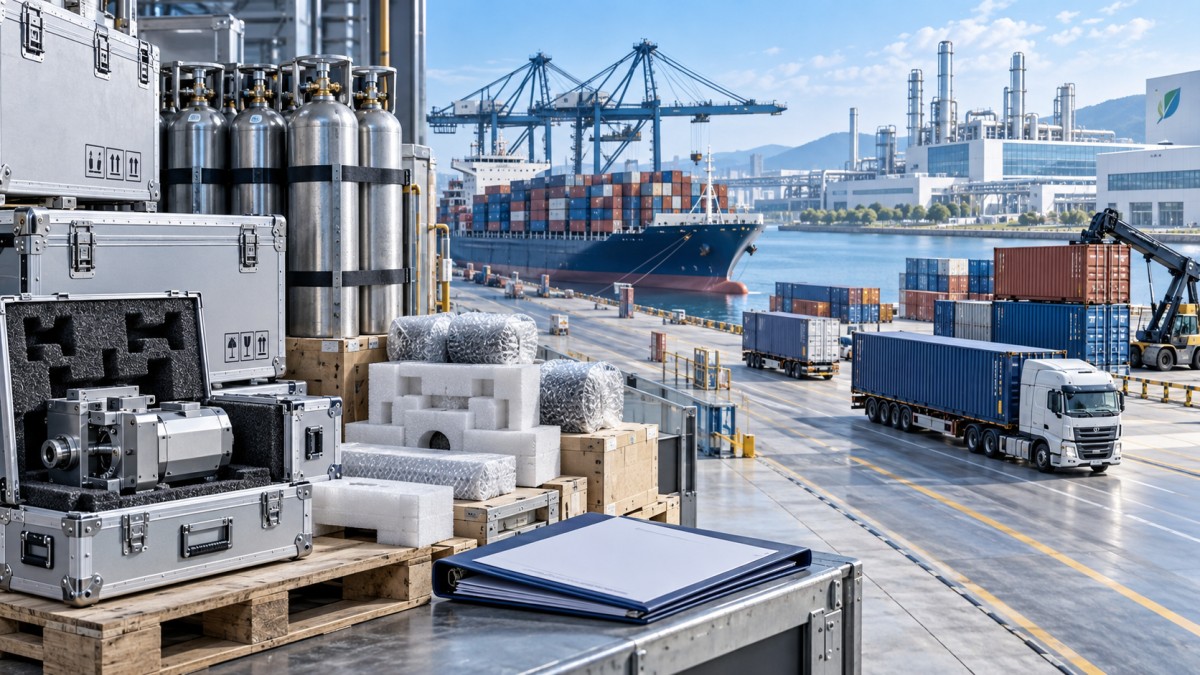
The map should also identify single points of failure. These are not limited to sole-source manufacturers. A product with two approved manufacturers can still have one approved logistics route, one qualified repair center, one customs broker familiar with the shipment classification, or one engineer authorized to perform installation acceptance.
Questions that expose hidden dependency
- Does the supplier hold finished stock, work-in-process stock, or only raw material?
- Can the supplier reserve capacity against a rolling forecast, or does each purchase order enter a general queue?
- Is the quoted lead time based on standard configuration, or does it exclude testing, documentation, export processing, and transit?
- Will a local distributor provide the same traceability and technical support as the original manufacturer?
- Which replacement parts are required to keep installed equipment operational, and where are they stocked?
- What happens when a shipment is held for clarification: who can provide the technical description, classification support, and documents promptly?
These questions shift procurement planning Latin America from a price comparison exercise toward a practical continuity assessment.
Segment purchases by consequence, not by annual spend alone
High spending does not automatically mean high supply risk, and a low-value seal, sensor, or fitting can stop an entire production cell. A useful planning model ranks items according to the consequence of non-availability, the difficulty of substitution, and the time required to restore supply.
One item can belong to more than one category. Electronic gases, for example, may be technically controlled because purity and container history matter, capacity constrained because supply is specialized, and trade-sensitive because shipping conditions and documentation must be correct. A simple spend-based purchasing rule will not capture that exposure.
Use supplier qualification as an ongoing control
Qualification is often mistaken for a one-time onboarding event. In a risk-sensitive supply chain, it should be maintained through structured evidence and regular review. The depth of review should match the item’s consequence. A supplier of noncritical office supplies does not need the same process as a supplier of deposition precursors or laser-interferometer-controlled positioning equipment.
For critical suppliers, buyers should confirm that the quoted configuration matches the approved technical baseline and that the supplier can preserve that baseline over time. Relevant evidence may include manufacturing controls, lot traceability, inspection or calibration capability, change-notification procedures, packaging methods, and the process used to manage nonconforming material. The objective is not to demand every possible document. It is to determine whether the supplier can consistently support the exact characteristics on which production depends.
Change control deserves special attention. A supplier may improve a process, replace a subcomponent, revise a software version, modify a coating method, or shift production to another site. Any of these changes can be harmless, beneficial, or unacceptable depending on the application. Procurement should define which changes require prior notice and which require engineering or quality reapproval. Without this rule, a buyer may discover variation only after incoming inspection, installation, or process qualification fails.
Plan import readiness before issuing the release
Import-related risk is often managed too late because the purchase order is viewed as the end of procurement’s responsibility. For critical material, the order release should trigger an import-readiness review. The review confirms that the shipment description is technically accurate, the commercial and shipping documents will align, and the receiving organization knows how the goods will be accepted, stored, and inspected.
Particular care is needed where product descriptions are vague. Labels such as “industrial equipment,” “laboratory material,” or “gas component” may be insufficient for customs processing or internal receipt. Documentation should describe the item consistently enough for commercial, transport, and technical teams to recognize the same product. Inconsistent quantities, units of measure, country-of-origin details, or part numbers can create avoidable delays.
Buyers should also establish the handoff points. Who verifies the packing list? Who receives safety documentation? Who confirms that a temperature-sensitive or hazardous shipment can be accepted on arrival? Who can answer technical questions raised by a customs broker or carrier? These responsibilities should be assigned before dispatch, not improvised while the cargo is waiting.
Incoterms require operational interpretation
Commercial delivery terms affect risk allocation, but they do not replace a delivery plan. Procurement needs to know who arranges freight, who controls carrier selection, who prepares export documents, who manages import clearance, and who is responsible for the shipment after it reaches a port or airport. A term that appears favorable on price can leave the buyer with limited visibility over the leg where the greatest delay occurs.
The right approach is to document the expected route and decision owners for each critical purchase. Where possible, retain enough shipment visibility to identify delays before they become line-stoppage events. This is especially important for equipment requiring coordinated installation, commissioning, or calibration after arrival.
Set inventory policy around recovery time
Safety stock is not a universal answer. Holding excess stock may create shelf-life exposure, storage hazards, working-capital pressure, or obsolescence risk. Yet avoiding inventory entirely can be equally dangerous when replenishment depends on overseas manufacturing, specialized freight, or technical release.
A stronger method compares the amount of stock on hand with the time required to recover from a disruption. Recovery time includes more than supplier production lead time. It can include technical approval, manufacturing queue time, testing, document preparation, export release, transport, customs clearance, domestic delivery, incoming inspection, and installation or calibration. For some items, the recovery path is longer than the quoted lead time by a meaningful margin.
Different controls suit different materials. A high-value instrument may need a defined spare-module strategy rather than duplicate full equipment. A critical consumable may need a reorder point tied to validated replenishment time. A material with a limited shelf life may require staggered releases and tighter forecast sharing instead of large inventory. The policy should reflect how the item fails, how quickly it can be replaced, and whether an alternate has already been technically accepted.
Make alternatives usable before the emergency
A backup supplier is not a contingency if the alternate part has never been reviewed, if its certificate format is unknown, or if the receiving team cannot inspect it against an agreed standard. Dual sourcing is valuable only when both sources are operationally qualified for the required application.
Where a direct alternate is not available, procurement can still create options. These may include an approved repair route, a regional stockholding arrangement, a substitute material for noncritical work, a temporary production sequence that reduces consumption, or a service agreement covering high-failure components. The key is to distinguish between an idea and an executable response. Each contingency should have a trigger, an owner, and an approval path.
For sensitive systems, engineering should participate early. A change from one coating source, gas grade, measurement probe, actuator, or motion-control configuration to another can affect process performance in ways that are not visible on a purchase order. Procurement provides the commercial and supply intelligence; engineering and quality determine the technical acceptance boundary.
Review leading signals instead of waiting for missed deliveries
Late deliveries are lagging indicators. By the time a purchase order is overdue, the choices may be limited to expediting, rescheduling, or accepting operational disruption. Planning works better when the team monitors signals that appear earlier in the supply path.
- Forecast demand is increasing while open supplier capacity has not been confirmed.
- A supplier repeatedly changes promised dates before shipment.
- Technical documents remain incomplete close to the planned dispatch date.
- A shipment is ready physically but lacks a required certificate, safety document, or export approval.
- Inventory is above minimum level, but most stock belongs to a lot nearing expiry or awaiting inspection.
- A sole-source component has no tested repair, replacement, or substitute path.
These signals should lead to specific actions: confirm capacity, request a document review, accelerate technical release, adjust the production plan, place a controlled buffer order, or begin alternate qualification. A monthly scorecard can help, but only if it links performance data to decisions. Recording supplier on-time delivery without reviewing root causes, route performance, quality holds, and document failures will not reduce future risk.
Use cross-functional planning at the points where supply can stop production
Procurement cannot manage all supply risk alone. The most useful planning reviews involve purchasing, production planning, engineering, quality, logistics, finance, and the teams responsible for receiving or handling controlled materials. The meeting does not need to cover every purchase. It should focus on items with an approaching shortage, an unresolved technical issue, a difficult import path, or a planned supplier change.
The value of this review is practical. Production planning can identify the date at which a shortage becomes operationally critical. Engineering can clarify whether an alternate is acceptable. Quality can define the incoming evidence needed for release. Logistics can verify route and receiving constraints. Procurement can then act on a complete picture rather than attempting to solve a late-order problem with only supplier follow-up.
Effective procurement planning in Latin America is therefore less about predicting every disruption and more about reducing the number of surprises that can halt a technically demanding operation. When requirements are clear, supply paths are mapped, documents are prepared early, alternatives are qualified, and recovery time is understood, procurement becomes a control point for continuity rather than a final administrative step.
Recent Articles
 2026.10.11How procurement planning reduces supply risk in Latin AmericaProcurement planning Latin America helps reduce supply risk with supplier qualification, import readiness, inventory controls, and contingency sourcing.
 2026.10.10How to build a supplier capability evaluation scorecard for critical partsSupplier capability evaluation scorecard: build a risk-based framework with gates, evidence, and weighted criteria to qualify critical-part suppliers with confidence.
 2026.10.09When do sub micron pneumatic actuators improve metrology repeatability?Sub micron pneumatic actuators for metrology improve repeatability by reducing friction, controlling contact force, and accelerating settling time. Discover when they deliver measurable inspection gains.
 2026.10.08How to assess measurement uncertainty from a precision metrology supplierPrecision metrology supplier guide: assess measurement uncertainty, traceability, environmental effects, calibration, and decision rules for reliable results.
 2026.10.07Metrology application notes for choosing CMM probe strategiesMetrology application notes for selecting CMM probe strategies, improving accuracy, access, repeatability, and confidence in complex feature inspection.
 2026.10.06What refresh rate do VR headsets need to reduce motion sicknessVR headsets need at least 90Hz to help reduce motion sickness. Discover why stable frame rates, low latency, and 120Hz support can deliver smoother, more comfortable VR experiences.
 2026.10.05What drives nano-indentation systems cost for a new lab?Nano-indentation systems cost: discover the real budget drivers for a new lab, from configuration and site readiness to software, calibration, and service.
 2026.10.04When does a micro fluidic probe OEM need custom channel geometry?Micro fluidic probe OEM guide: learn when custom channel geometry improves confinement, shear control, reagent savings, and process reliability.
 2026.10.03How to prevent cross-contamination in semiconductor gas handlingSemiconductor Gas Handling best practices to prevent cross-contamination, protect gas purity, improve process stability, and strengthen fab safety.
 2026.10.02How healthcare engineering improves the accuracy of diagnostic equipmentHealthcare engineering improves diagnostic accuracy through precision design, calibration, fluid control, and traceable validation for reliable clinical results.
 2026.10.01When does a steel-frame vibration isolation table provide enough stability?Vibration isolation table steel frame stability explained: assess stiffness, resonance, payload, and isolator performance for precise, reliable measurements.
 2026.09.30How probe station procurement alerts prevent costly supply delaysProbe station procurement alerts help teams spot configuration risks, lead-time changes, and compliance issues early—protecting test schedules and avoiding costly supply delays.
 2026.09.29What Maintenance Does a Micro-Manipulation System Need?What maintenance does a micro-manipulation system need? Explore calibration, cleaning, motion checks, cable care, and environmental controls for reliable precision.
 2026.09.29Microdynamics in Precision Motion: What Engineers Need to MeasureMicrodynamics in precision motion: learn what engineers must measure to control vibration, settling, friction, compliance, and servo response for reliable nanometer-level results.
 2026.09.29OEM Nanopositioning Solutions: Specifying Travel, Load, and Control RequirementsOEM nanopositioning solutions guide: specify usable travel, real payload dynamics, feedback, and control integration for reliable precision instruments.
 2026.09.29Factory-Price Photoresist Chemicals: What Buyers Should Verify Before OrderingFactory price photoresist chemicals: learn the essential checks for process fit, lot control, purity, packaging, and total cost before ordering.
 2026.09.29When Does Laser Interferometer Precision Limit a Metrology System?Laser interferometer precision: learn when it limits metrology systems, from air-path effects and alignment errors to uncertainty budgets and smarter upgrades.
 2026.09.29Selecting a Semi-Automatic Wafer Prober for Low-Volume Test LinesChoose a semi automatic wafer prober for low-volume test lines with guidance on contact stability, flexible wafer handling, probe compatibility, and repeatable workflows.
 2026.09.29Piezo Valves for Fast Gas Dosing: Matching Response Time to Process NeedsPiezo valves for fast gas dosing: learn how to match response time, pressure conditions, and system design for stable, repeatable process control.
 2026.09.29Why a Piezo Valve Loses Repeatability—and How to Diagnose ItPiezo valve repeatability issues? Learn how to diagnose drive signals, contamination, pressure instability, bubbles, and wear before costly replacement.
 2026.09.29Nanopositioning Stages: Comparing Direct-Drive and Piezo-Flexure DesignsNanopositioning stages compared: explore direct-drive and piezo-flexure designs for travel, stiffness, settling time, thermal stability, and precision control.
 2026.09.29ArF Photoresist in Vietnam: Supply-Chain Risks for Semiconductor FabsArF photoresist in Vietnam: uncover supply-chain, compliance, logistics, and qualification risks. Build resilient sourcing strategies for semiconductor fabs.
 2026.09.29Ultra-Pure Silane Gas in the Middle East: Purity and Delivery ChecksUltra-pure silane gas Middle East acceptance guide: verify purity, CoA traceability, cylinder integrity, and safe delivery controls for critical processes.
 2026.09.29How Web Tension and Oven Zoning Affect Coating Calendering Line QualityCoating calendering line quality depends on stable web tension and precise oven zoning. Learn how to reduce gloss, gauge, adhesion, and embossing defects.
 2026.09.29How high stability optical tweezers reduce drift in long experimentsOptical tweezers high stability systems reduce long-experiment drift through rigid mechanics, thermal control, low-noise optics, and meaningful feedback. Explore evaluation methods.
 2026.09.28How piezo polymer materials affect sensitivity in flexible sensorsPiezo polymer materials shape flexible sensor sensitivity. Explore stress transfer, film stability, electronics, and testing insights for reliable high-performance designs.
 2026.09.27When does recyclable skincare packaging justify its higher unit cost?Skincarepackaging costs more only when it protects formulas, supports credible recycling claims, reduces compliance risk, and delivers measurable commercial value.
 2026.09.26How to choose a hiking backpack that fits your torso lengthHikingbackpacks fitting guide: measure your torso, adjust hip belts and straps, and choose a stable, comfortable pack for every trail adventure.
 2026.09.25Which ISO standards apply to precision-engineered medical devices?ISO standards for precision engineering medical devices: explore ISO 13485, ISO 14971, metrology, biocompatibility, sterilization, and packaging requirements.
 2026.09.24How to choose athletic clothing that stays comfortable in humid weatherAthletic clothing for humid weather: learn how to choose breathable fabrics, low-chafe fits, and quick-drying layers for more comfortable workouts.
 2026.09.23How sheet metal welding choices affect dimensional accuracySheet metal welding choices shape dimensional accuracy. Explore heat input, joint design, fixturing, and inspection strategies to reduce distortion and improve repeatability.
 2026.09.22How specification preparation prevents flow-control errors in process systemsSpecification preparation for process systems prevents flow-control errors by defining operating ranges, pressure budgets, accuracy, materials, and control requirements before equipment selection.
 2026.09.21How to assess a German mass flow controller supplier for cleanroom useIndustrial & Manufacturing equipment supplier in Germany: assess cleanroom MFC partners for gas compatibility, leak integrity, calibration traceability, and lifecycle service.
 2026.09.20How to assess aerospace component manufacturing services for tight tolerancesAerospace component manufacturing services: learn how to verify tight-tolerance capability through metrology, process control, special-process oversight, and traceability.
FILTER_CORE
REF_NO: 0042
Editors' Picks
- 00
0000-00
How procurement planning reduces supply risk in Latin America - 00
0000-00
How to build a supplier capability evaluation scorecard for critical parts - 00
0000-00
When do sub micron pneumatic actuators improve metrology repeatability? - 00
0000-00
How to assess measurement uncertainty from a precision metrology supplier