What Should a Precision Manufacturing Supplier Audit Include?
What Should a Precision Manufacturing Supplier Audit Include?
What should be included in a precision manufacturing supplier audit? For a buyer sourcing ordinary machined parts, the answer may begin with capacity, price, and delivery performance. For aerospace hardware, semiconductor tooling, medical components, precision fluid-control assemblies, or nano-positioning systems, that approach is incomplete. A supplier can own impressive machines, hold familiar certificates, and still be unable to produce a stable process for the tolerance, cleanliness, material condition, or documentation package your project requires.
A useful audit is not a factory tour with a checklist. It is an effort to determine whether a supplier can repeatedly convert a drawing, specification, or functional requirement into conforming product under real production conditions. That distinction matters. The best-looking first article is not proof of repeatability, and a quality manual is not proof that operators, measurement systems, subcontractors, and change-control practices are working together.
In ultra-precision procurement, the audit should follow the actual risk path of the component: material receipt, process planning, machining or deposition, cleaning, inspection, handling, packaging, release, and traceability. It should also examine the supplier’s ability to respond when a result drifts—not merely its ability to report that it drifted.
Start with the part’s real critical characteristics
Before auditing a supplier, define what “precision” means for the purchase. A general tolerance on a drawing tells only part of the story. The truly consequential requirements may be a datum relationship, surface integrity after grinding, burr control inside a small fluid path, particle contamination, coating adhesion, residual stress, material lot traceability, or long-term positional stability.
This is where many supplier evaluations become too generic. A shop may demonstrate excellent dimensional capability on robust steel components but have limited control over thin-wall parts, freeform optics, difficult alloys, miniature features, or parts that must remain clean enough for vacuum, semiconductor, or medical use. Ask the supplier to explain how it identifies critical-to-quality features and how those features are reflected in process planning, inspection frequency, and release criteria.
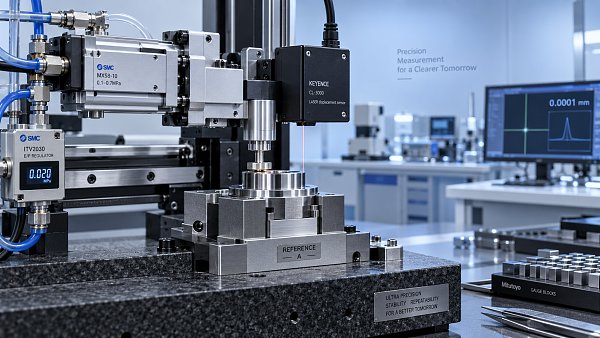
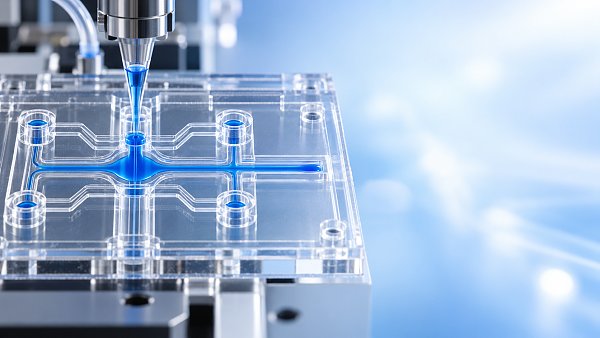
For complex assemblies, audit the interfaces as carefully as the individual parts. A precision pneumatic actuator, for example, may fail functional testing because of sealing-surface damage, particulate contamination, assembly force variation, or a purchased component that meets its own drawing but not the system requirement. Dimensional conformance alone does not close that risk.
Process capability: look beyond machine names
A supplier audit should verify whether the proposed manufacturing route is appropriate for the required tolerance and production volume. Equipment lists are useful, but they are only a starting point. The more relevant questions are practical: Which machine will run the work? Is it dedicated, shared, or frequently interrupted by lower-priority jobs? What workholding is used? How is thermal variation managed? How often are tools changed? Which process parameters are locked, recorded, or left to operator judgment?
For a tight geometry, it is reasonable to ask for evidence from comparable work, while recognizing that “comparable” must mean more than a similar nominal size. Material behavior, feature accessibility, wall thickness, batch size, and inspection method can all change the outcome. A supplier that cannot disclose customer drawings may still be able to show anonymized process studies, setup instructions, in-process control plans, or representative inspection data.
Pay particular attention to special processes. Heat treatment, welding, plating, passivation, thin-film deposition, laser processing, cleaning, and coating operations can alter dimensions or material performance after machining is complete. If the supplier outsources these steps, the audit needs to follow the control chain outside the building. “Approved subcontractor” is not enough; buyers should understand who validates the subcontractor, how lots are identified, what acceptance evidence is received, and how process changes are communicated.
Metrology must be matched to the requirement
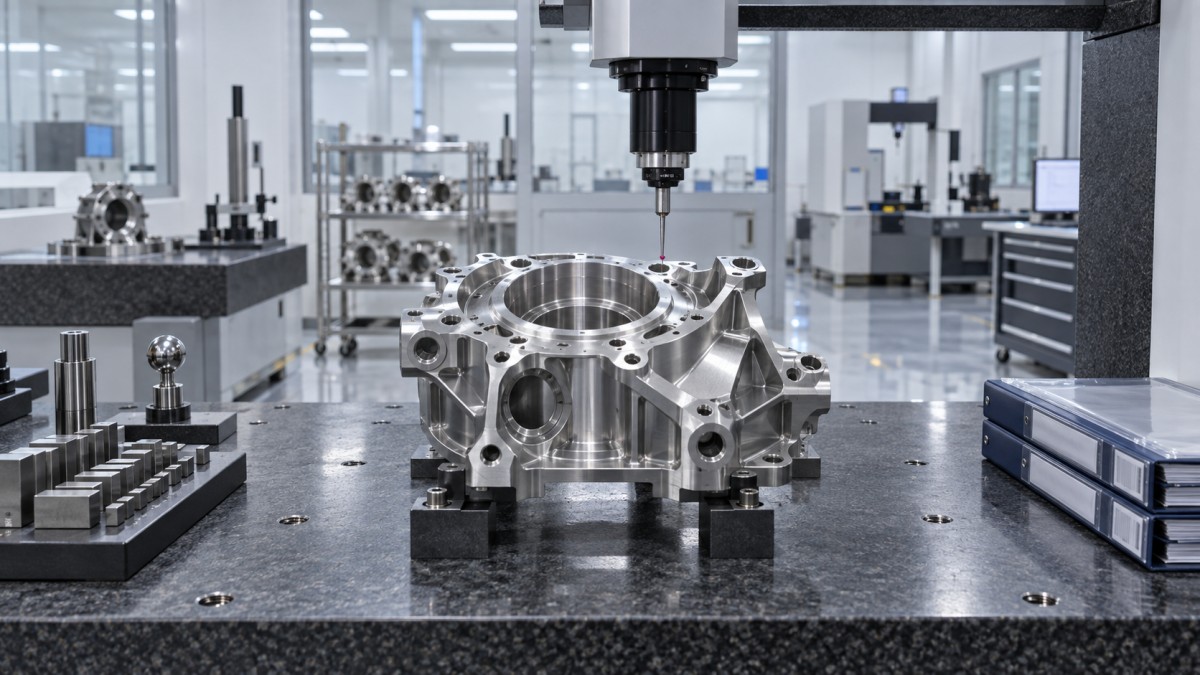
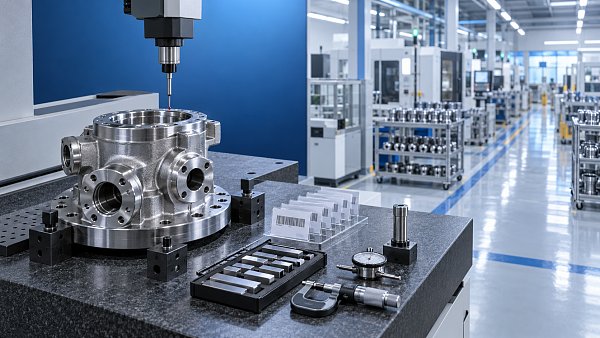
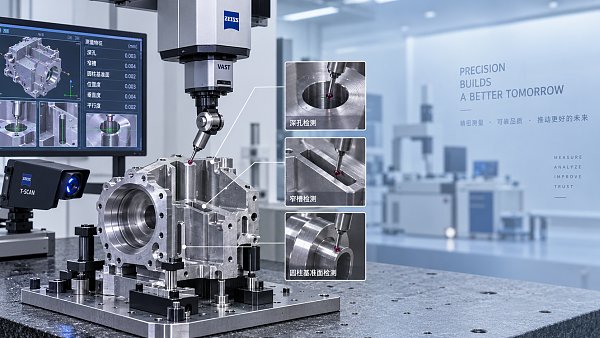
Precision manufacturing lives or dies on measurement credibility. A coordinate measuring machine can be highly capable, but it is not automatically the right instrument for every feature. Surface texture, micro-feature geometry, roundness, coating thickness, optical alignment, leak performance, and sub-micron motion behavior may require different methods, environments, fixtures, or specialist expertise.
During the audit, inspect the measurement plan rather than simply confirming that a metrology room exists. Is the datum scheme consistent between drawing interpretation, machining setup, and final inspection? Are fixtures designed to avoid deforming sensitive parts? Is the inspection sequence sensible? Can the chosen instrument resolve the tolerance with enough margin to support a confident acceptance decision? A supplier should be able to discuss the limitations of its method, not just its nominal equipment accuracy.
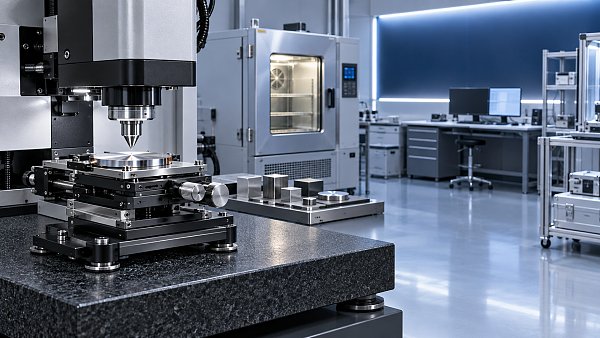
Traceability also deserves a direct check. Calibration labels are visible, but the deeper issue is whether measurement equipment is calibrated through a documented system with traceability appropriate to the application. Environmental conditions matter as well. Temperature control, vibration, cleanliness, and handling practices can influence results, especially where CMM, multi-sensor metrology, interferometry, or high-magnification optical inspection is involved.
A sensible audit asks how the supplier reacts when inspection results disagree. Do engineers investigate fixturing, programming, datum interpretation, and material movement? Or does the team simply remeasure until a preferred result appears? The answer often reveals more about quality culture than a polished calibration register.
Follow material and documentation from receipt to shipment
For safety-critical or regulated applications, material paperwork is not an administrative afterthought. The audit should establish whether incoming material is identified, segregated, verified against the purchase requirement, and linked to the finished lot. This may include mill or material certificates where contractually required, incoming inspection records, shelf-life controls, storage conditions, and rules for preserving identity after material is cut into smaller pieces.
The same principle applies to high-purity chemicals, electronic gases, coatings, adhesives, and consumables. Their handling requirements may be as important as their nominal specification. In semiconductor-adjacent work, for instance, a technically correct material can still create a problem if its contamination history, storage practice, or change notification is unclear.
Ask to trace one completed production lot backwards. The supplier should be able to connect the shipment to the work order, operator or machine records where relevant, inspection results, material source, nonconformance disposition, and any external processing. Then reverse the exercise: take an incoming material lot and ask which finished units received it. Gaps become obvious quickly when traceability is tested this way.
Audit quality controls where production pressure is highest
Most suppliers can describe corrective action procedures. The harder question is whether those procedures work when schedules are tight, a key machine is down, or a nonconforming batch is already near shipment. Review a small sample of closed nonconformances if access is permitted. Look for a clear containment action, an analysis tied to evidence, correction of the process rather than only the immediate part, and confirmation that the action was effective.
Change control deserves equal attention. A change in cutting tool, software revision, material source, coating house, inspection program, cleaning chemistry, or packaging method may be harmless—or it may affect a critical characteristic. The supplier should have a defined way to evaluate changes and know when customer notification or requalification is required. This is particularly important for components used in qualified aerospace, medical, semiconductor, or laboratory systems.
Certification can provide useful structure. Depending on the product and market, buyers may review alignment with applicable ISO quality systems, sector-specific requirements, customer specifications, or standards associated with SEMI and IEEE environments. But a certificate should never substitute for a project-specific audit. Scope, site coverage, exclusions, and the practical maturity of the process all need verification.
Assess people, production discipline, and knowledge retention
Ultra-precision work remains unusually dependent on experienced people. A programmed machine does not remove the need for sound judgment in fixturing, toolpath strategy, deburring, cleaning, inspection, or handling. During a site visit, observe whether setup instructions are current and accessible, whether operators understand critical features, and whether experienced knowledge has been converted into controlled documentation.
One warning sign is a process that depends on one specialist “who knows how to make it work.” That person may be excellent, but the supply risk is real if the process cannot be reproduced during absence, turnover, or capacity expansion. Cross-training, controlled work instructions, and technical review routines are more valuable than a vague assurance that the supplier employs skilled machinists.
Do not separate technical capability from supply-chain resilience
A precision supplier can be technically qualified and still be commercially fragile. Audit capacity planning, equipment maintenance, dependency on single-source subcontractors, lead times for critical materials, and recovery planning for machine failure or quality escapes. There is no universal acceptable level of redundancy; a prototype program and a long-term production platform carry different expectations. What matters is whether the supplier can describe its exposure honestly and whether the buyer has a workable contingency plan.
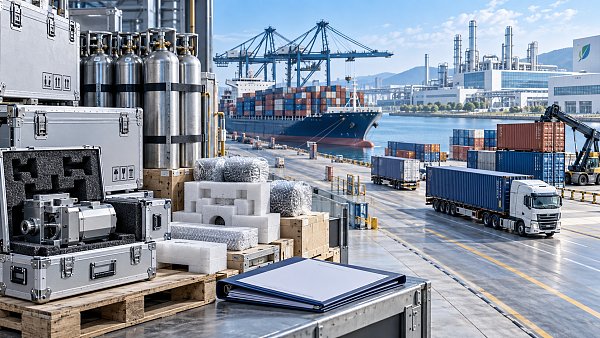
Cross-border sourcing introduces further checks. Export controls, technical-data access, country-of-origin requirements, and restricted substances may affect a project even when the machined part itself appears uncomplicated. These topics should be reviewed early with the relevant legal, trade-compliance, and engineering stakeholders. A late discovery can delay qualification more than any ordinary production issue.
This is one reason multidisciplinary benchmarking is useful. In fields spanning specialized coatings, precision fluid control, CMM and multi-sensory metrology, ultra-high-purity chemicals, and nano-positioning systems, a supplier’s capability cannot be judged from a single specification sheet. Technical performance, measurement confidence, regulatory awareness, and supply-chain visibility must be considered together. Platforms such as Global Ultra-Precision Engineering focus on making those comparisons more evidence-led, particularly where international standards and rapidly changing technical requirements intersect.
Turn the audit into a qualification decision
The final audit report should not simply score a supplier as “approved” or “not approved.” It should identify which parts, tolerances, materials, processes, and volumes the supplier is qualified to support—and where the boundaries are. A supplier may be suitable for development quantities but not yet for serial production. Another may be strong in machining but require additional validation for cleaning, coating, or final assembly. Those distinctions protect both parties from an overbroad approval.
The most reliable next step is usually a controlled pilot: a representative first article, defined inspection package, agreed documentation, and a review of actual process performance before broader release. A good audit does not eliminate risk. It makes risk visible early enough to manage it, before a difficult component becomes a delayed program or a costly field problem.
Taglist:
- Ultra-Precision Engineering
- Specialized Coatings
- Thin-Film Deposition
- Precision Pneumatic
- Fluid Control
- Multi-Sensory Metrology
- Electronic Gases
- Nano-Positioning
- Precision Manufacturing
- precision fluid control
- nano-positioning systems
- Precision Manufacturing supplier
- Precision Pneumatic actuator
- measurement systems
- multi-sensor metrology
- What should be included in a precision manufacturing supplier audit?
Recent Articles
 2026.10.13How to choose a packaging manufacturer for small production runsChoose a packaging manufacturer for small production runs with confidence. Discover how to compare costs, verify samples, and secure quality packaging without excess inventory.
 2026.10.12How to size commercial refrigerators for a restaurant kitchenDiscover how commercialrefrigerators should be sized for peak demand, smarter workflow, food safety, and reliable restaurant kitchen performance.
 2026.10.11How procurement planning reduces supply risk in Latin AmericaProcurement planning Latin America helps reduce supply risk with supplier qualification, import readiness, inventory controls, and contingency sourcing.
 2026.10.10How to build a supplier capability evaluation scorecard for critical partsSupplier capability evaluation scorecard: build a risk-based framework with gates, evidence, and weighted criteria to qualify critical-part suppliers with confidence.
 2026.10.09When do sub micron pneumatic actuators improve metrology repeatability?Sub micron pneumatic actuators for metrology improve repeatability by reducing friction, controlling contact force, and accelerating settling time. Discover when they deliver measurable inspection gains.
 2026.10.08How to assess measurement uncertainty from a precision metrology supplierPrecision metrology supplier guide: assess measurement uncertainty, traceability, environmental effects, calibration, and decision rules for reliable results.
 2026.10.07Metrology application notes for choosing CMM probe strategiesMetrology application notes for selecting CMM probe strategies, improving accuracy, access, repeatability, and confidence in complex feature inspection.
 2026.10.06What refresh rate do VR headsets need to reduce motion sicknessVR headsets need at least 90Hz to help reduce motion sickness. Discover why stable frame rates, low latency, and 120Hz support can deliver smoother, more comfortable VR experiences.
 2026.10.05What drives nano-indentation systems cost for a new lab?Nano-indentation systems cost: discover the real budget drivers for a new lab, from configuration and site readiness to software, calibration, and service.
 2026.10.04When does a micro fluidic probe OEM need custom channel geometry?Micro fluidic probe OEM guide: learn when custom channel geometry improves confinement, shear control, reagent savings, and process reliability.
 2026.10.03How to prevent cross-contamination in semiconductor gas handlingSemiconductor Gas Handling best practices to prevent cross-contamination, protect gas purity, improve process stability, and strengthen fab safety.
 2026.10.02How healthcare engineering improves the accuracy of diagnostic equipmentHealthcare engineering improves diagnostic accuracy through precision design, calibration, fluid control, and traceable validation for reliable clinical results.
 2026.10.01When does a steel-frame vibration isolation table provide enough stability?Vibration isolation table steel frame stability explained: assess stiffness, resonance, payload, and isolator performance for precise, reliable measurements.
 2026.09.30How probe station procurement alerts prevent costly supply delaysProbe station procurement alerts help teams spot configuration risks, lead-time changes, and compliance issues early—protecting test schedules and avoiding costly supply delays.
 2026.09.29What Should a Precision Manufacturing Supplier Audit Include?What should be included in a precision manufacturing supplier audit? Explore essential checks for process capability, metrology, traceability, and risk control.
 2026.09.29How Do Export Controls Affect Semiconductor Equipment Lead Times?How do export controls affect semiconductor equipment lead times? Discover licensing, screening, supplier, and service risks—and plan smarter to protect fab schedules.
 2026.09.29What Maintenance Does a Micro-Manipulation System Need?What maintenance does a micro-manipulation system need? Explore calibration, cleaning, motion checks, cable care, and environmental controls for reliable precision.
 2026.09.29Microdynamics in Precision Motion: What Engineers Need to MeasureMicrodynamics in precision motion: learn what engineers must measure to control vibration, settling, friction, compliance, and servo response for reliable nanometer-level results.
 2026.09.29OEM Nanopositioning Solutions: Specifying Travel, Load, and Control RequirementsOEM nanopositioning solutions guide: specify usable travel, real payload dynamics, feedback, and control integration for reliable precision instruments.
 2026.09.29Factory-Price Photoresist Chemicals: What Buyers Should Verify Before OrderingFactory price photoresist chemicals: learn the essential checks for process fit, lot control, purity, packaging, and total cost before ordering.
 2026.09.29When Does Laser Interferometer Precision Limit a Metrology System?Laser interferometer precision: learn when it limits metrology systems, from air-path effects and alignment errors to uncertainty budgets and smarter upgrades.
 2026.09.29Selecting a Semi-Automatic Wafer Prober for Low-Volume Test LinesChoose a semi automatic wafer prober for low-volume test lines with guidance on contact stability, flexible wafer handling, probe compatibility, and repeatable workflows.
 2026.09.29Piezo Valves for Fast Gas Dosing: Matching Response Time to Process NeedsPiezo valves for fast gas dosing: learn how to match response time, pressure conditions, and system design for stable, repeatable process control.
 2026.09.29Why a Piezo Valve Loses Repeatability—and How to Diagnose ItPiezo valve repeatability issues? Learn how to diagnose drive signals, contamination, pressure instability, bubbles, and wear before costly replacement.
 2026.09.29Nanopositioning Stages: Comparing Direct-Drive and Piezo-Flexure DesignsNanopositioning stages compared: explore direct-drive and piezo-flexure designs for travel, stiffness, settling time, thermal stability, and precision control.
 2026.09.29ArF Photoresist in Vietnam: Supply-Chain Risks for Semiconductor FabsArF photoresist in Vietnam: uncover supply-chain, compliance, logistics, and qualification risks. Build resilient sourcing strategies for semiconductor fabs.
 2026.09.29Ultra-Pure Silane Gas in the Middle East: Purity and Delivery ChecksUltra-pure silane gas Middle East acceptance guide: verify purity, CoA traceability, cylinder integrity, and safe delivery controls for critical processes.
 2026.09.29How Web Tension and Oven Zoning Affect Coating Calendering Line QualityCoating calendering line quality depends on stable web tension and precise oven zoning. Learn how to reduce gloss, gauge, adhesion, and embossing defects.
 2026.09.29How high stability optical tweezers reduce drift in long experimentsOptical tweezers high stability systems reduce long-experiment drift through rigid mechanics, thermal control, low-noise optics, and meaningful feedback. Explore evaluation methods.
 2026.09.28How piezo polymer materials affect sensitivity in flexible sensorsPiezo polymer materials shape flexible sensor sensitivity. Explore stress transfer, film stability, electronics, and testing insights for reliable high-performance designs.
 2026.09.27When does recyclable skincare packaging justify its higher unit cost?Skincarepackaging costs more only when it protects formulas, supports credible recycling claims, reduces compliance risk, and delivers measurable commercial value.
 2026.09.26How to choose a hiking backpack that fits your torso lengthHikingbackpacks fitting guide: measure your torso, adjust hip belts and straps, and choose a stable, comfortable pack for every trail adventure.
 2026.09.25Which ISO standards apply to precision-engineered medical devices?ISO standards for precision engineering medical devices: explore ISO 13485, ISO 14971, metrology, biocompatibility, sterilization, and packaging requirements.
 2026.09.24How to choose athletic clothing that stays comfortable in humid weatherAthletic clothing for humid weather: learn how to choose breathable fabrics, low-chafe fits, and quick-drying layers for more comfortable workouts.
FILTER_CORE
REF_NO: 0042
Editors' Picks