Why do semiconductor materials need lot traceability? For semiconductor PVD targets, the answer lies in protecting wafer yield and connecting thin-film performance to verifiable material records.
A purity deviation, microstructural inconsistency, or bonding defect can disrupt deposition stability. Identifying its source requires manufacturing evidence, inspection results, and records connecting targets to production.
For procurement directors, process engineers, and supplier quality teams, traceability supports three practical decisions: whether to release a target, investigate a deviation, or quarantine related inventory.
The strongest systems connect material genealogy to actual chamber use. A certificate alone cannot establish which wafers encountered a suspect target or explain the failure mechanism.
What Must a Traceable PVD Target Connect?
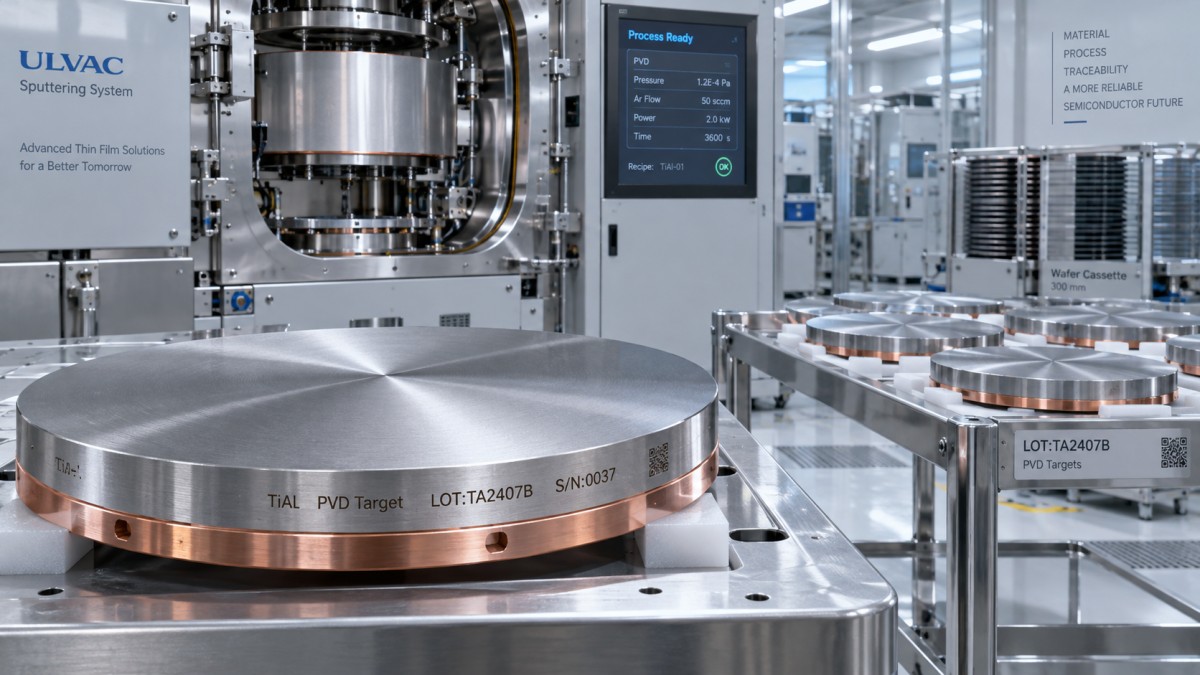
Lot traceability is the ability to follow a target backward through its manufacturing history and forward through shipment, installation, use, and any subsequent quality investigation.
Backward traceability identifies contributing feedstock batches, refining or consolidation steps, thermal processing, machining, cleaning, and inspection. Bonded assemblies also require links to backing plates and bonding operations.
Forward traceability identifies customers, shipments, storage locations, installed chambers, and affected production windows. Within the fab, installation records must connect the target to relevant wafer processing.
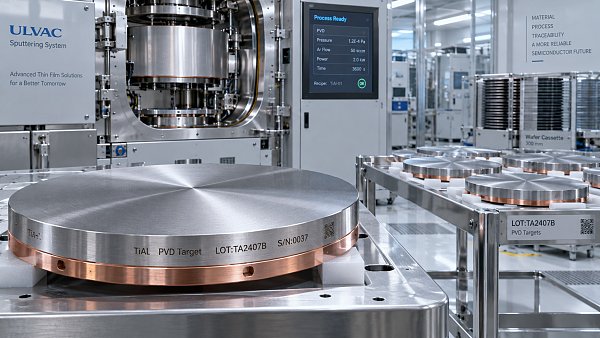
A lot number identifies a defined production group; a serial number identifies an individual target or assembly. Effective traceability often requires both levels of identification.
The supplier must explain how it defines a lot. One melt, one powder blend, one heat-treatment batch, and one shipment represent different boundaries for investigation.
Splitting a material batch into several targets should preserve the parent relationship. Combining feedstock batches should preserve every contributing source rather than replacing their identities.
Rebonding, rework, or other approved refurbishment must also remain visible. An unchanged serial number should never conceal a changed assembly configuration or revised inspection status.
The practical test is simple: can both organizations reconstruct a target’s history and locate related inventory quickly, without relying on individual employees’ memories or informal spreadsheets?
Which Target Problems Can Put Wafer Yield at Risk?
PVD targets supply the material deposited onto wafers. Their chemistry, internal structure, surface condition, and assembly integrity can influence deposition behavior alongside chamber hardware and recipes.
Unwanted metallic impurities may alter film properties or introduce contamination. Their significance depends on the deposited material, device application, impurity species, and the fab’s acceptance limits.
A headline purity value can obscure important differences between targets. Buyers need defined impurity limits, analytical methods, and reporting limits relevant to the intended process.
For alloy targets, composition consistency also matters. Meeting an average composition requirement does not automatically demonstrate acceptable uniformity across the target or throughout its usable volume.
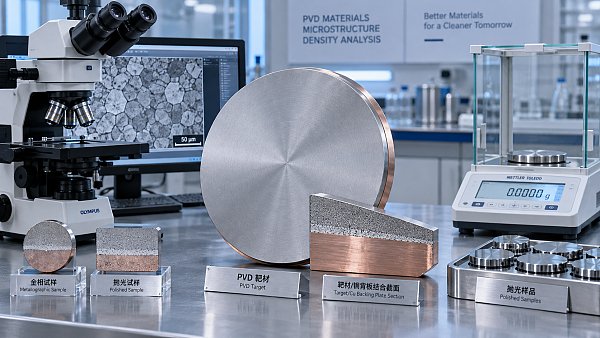
Grain structure, crystallographic texture, porosity, and inclusions can influence erosion behavior and deposition consistency. Their importance varies with target material, manufacturing route, and sputtering conditions.
In bonded targets, inadequate bond integrity can impair heat transfer. Under operating load, localized heating may contribute to instability, mechanical damage, or premature assembly failure.
Particles and arcing can have multiple causes, including chamber conditions, process settings, and target characteristics. Traceability helps test these possibilities; it does not establish causation alone.
This distinction matters commercially. Evidence linking a deviation to shared material or processing history supports targeted containment, while weak records can force a much broader production hold.
What Records Should Procurement Require Beyond a Certificate?
A certificate of analysis provides useful release evidence, but it usually summarizes selected results. Procurement should specify the underlying traceability records needed for qualification and investigations.
Requirements should distinguish records delivered with every shipment from records retained by the supplier. Sensitive manufacturing details can remain controlled while still being available for investigation.
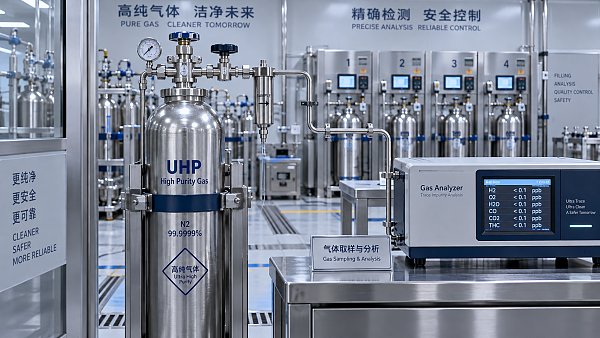
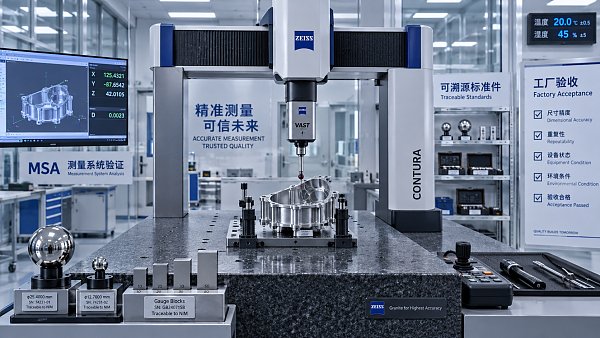
Analytical results should identify the method used and its relevant reporting limits. A reported absence of contamination is meaningful only within the capabilities of that method.
Sampling location and frequency also affect interpretation. A test on representative feedstock does not necessarily establish every property of each finished target or bonded assembly.
For microstructural requirements, specify the measurement approach and acceptance basis. Terms such as “fine grain” or “high density” provide insufficient evidence without agreed definitions and results.
For bonded assemblies, request inspection appropriate to the design and operating conditions. The supplier should explain what its inspection detects and which areas it evaluates.
Approved deviations must remain linked to the affected units. Procurement and engineering should be able to distinguish standard product from material released under a documented concession.
Retention periods should cover storage, service life, and the agreed investigation window. Retrieval expectations matter equally: retained records offer limited value when access takes weeks.
How Do Target Records Connect to Affected Wafers?
Supplier genealogy ends before wafer processing begins. The fab must extend the chain by recording which target entered which chamber and when processing occurred there.
At installation, capture the target serial number, material lot, chamber identity, installation time, and relevant assembly details. Verify these entries against physical labels and receiving records.
Link installation to conditioning, maintenance, recipe revisions, and production history. These events help distinguish material variation from changes in chamber state or process execution over time.
At removal, record the time, reason, accumulated usage, and observed condition. Relevant photographs or inspection findings can strengthen comparisons between suspect targets and unaffected units.
Wafer exposure should be determined from actual processing records. Shared material genealogy identifies candidates for review, while chamber history establishes which production lots were potentially exposed.
A single target lot may operate successfully in several chambers while one chamber experiences defects. That pattern warrants investigation of local conditions alongside the target’s history.
Conversely, similar deviations across different chambers using related targets strengthen the case for investigating shared feedstock, manufacturing steps, or assembly processes as possible contributing factors.
Connected records therefore support better judgment. They narrow the investigation while preserving enough context to avoid attributing every deposition problem to the target supplier prematurely.
What Should Happen When a Suspect Lot Is Found?
Consider a hypothetical increase in particle defects after installation of a new target. The immediate priority is controlling exposure while preserving evidence for a structured investigation.
The fab identifies the installed serial number, pauses affected use as appropriate, and reviews wafer processing since installation. It also checks chamber maintenance and recipe history.
The supplier retrieves the target’s genealogy and inspection records. Investigators then identify other targets sharing potentially relevant feedstock, consolidation, machining, cleaning, or bonding operations within the investigation.
Containment scope should follow the suspected mechanism. A bonding concern may implicate one assembly batch; a feedstock impurity concern may extend across several manufacturing and shipment lots.
Uninstalled inventory can be located and held while evidence develops. Already installed targets may require additional review, monitoring, or removal according to the fab’s risk assessment.
Comparisons should include unaffected targets where possible. Differences in chemistry, inspection results, chamber conditions, and operating history help determine which explanations remain credible after initial review.
Traceability also preserves evidence for corrective action. Supplier changes, revised acceptance criteria, or additional inspections should address the demonstrated failure mechanism rather than an assumed cause.
Release from containment requires documented justification and appropriate authorization. Closing the investigation should update affected records so future receiving and installation decisions reflect the final disposition.
How Can Buyers Verify a Supplier’s Traceability Capability?
Ask the supplier to demonstrate genealogy for a randomly selected shipped target. A prepared example may show system design without demonstrating consistent execution across routine production.
The demonstration should connect the delivered serial number to parent material, manufacturing batches, inspections, disposition, and shipment. Request explanations for any missing links or ambiguous identifiers.
Then reverse the exercise: select a parent material batch and ask which finished targets consumed it. This tests whether the supplier can identify the full affected population.
Include a reworked or rebonded assembly if those services are supplied. The record should preserve original identity, subsequent operations, renewed inspection, and final approval for shipment.
Evaluate retrieval speed against your operational needs. An agreed response time is more useful than a general promise that records are available whenever an incident occurs.
Check how identifiers survive packaging changes, relabeling, and warehouse transfers. Physical markings and electronic records must remain consistent without compromising target cleanliness or approved handling requirements.
Certifications can support confidence in a quality system, but they do not establish every required genealogy link. Verify compliance against applicable standards, contracts, and customer specifications.
Warning signs include shipment numbers presented as manufacturing lots, inaccessible underlying test records, undocumented substitutions, and inability to identify sibling targets produced from shared source material.
How Much Traceability Is Worth Paying For?
The appropriate investment depends on failure consequences, material sensitivity, target design, and production exposure. Expensive products or critical film applications generally justify more detailed evidence requirements.
Traceability creates value by shortening investigations and narrowing containment. Its return includes avoided production delays, reduced unnecessary inventory holds, and less engineering effort reconstructing missing information.
Estimate the business case using realistic incident scenarios. Compare record-management costs with the likely cost of chamber downtime, wafer review, target replacement, and supplier investigation delays.
Do not assume that more testing always produces better traceability. Testing evaluates selected characteristics; genealogy establishes relationships. Both need requirements matched to the actual failure risks.
A practical starting point is reliable lot and serial identification, accessible release evidence, documented parent relationships, and consistent chamber installation records supported by a tested retrieval process.
More advanced systems can automate these links, but software cannot repair ambiguous lot definitions or incomplete source records. Improve data quality before expanding dashboards and integrations.
What Should Buyers Conclude About PVD Target Lot Traceability?
Semiconductor PVD targets need lot traceability because material acceptance, wafer exposure, and incident containment depend on knowing exactly what was supplied and where it was used.
The buying decision should therefore consider evidence quality alongside purity, dimensions, performance, and price. A compliant specification has greater practical value when its supporting history is retrievable.
Require a supplier to demonstrate complete genealogy, define record access expectations, and connect target identity to fab usage. These steps make traceability useful during actual production problems.
Traceability cannot guarantee defect-free deposition. It gives procurement and engineering teams the evidence needed to investigate uncertainty, contain risk proportionately, and make better-informed release and supplier decisions.